These three principles come from what a hotend goes through.
It is knocked, wrenched and scrubbed.
Heat makes its metal grow.
Through all of it, it must stay stable and strong.
At speed, the plastic drains its heat.
It needs room to melt, and the power to keep up.
Years wear everything down.
So it is made of materials that endure, with spare parts found anywhere.
Stable as heat expands the metal.
Without losing print height.
Maintained with standard parts.
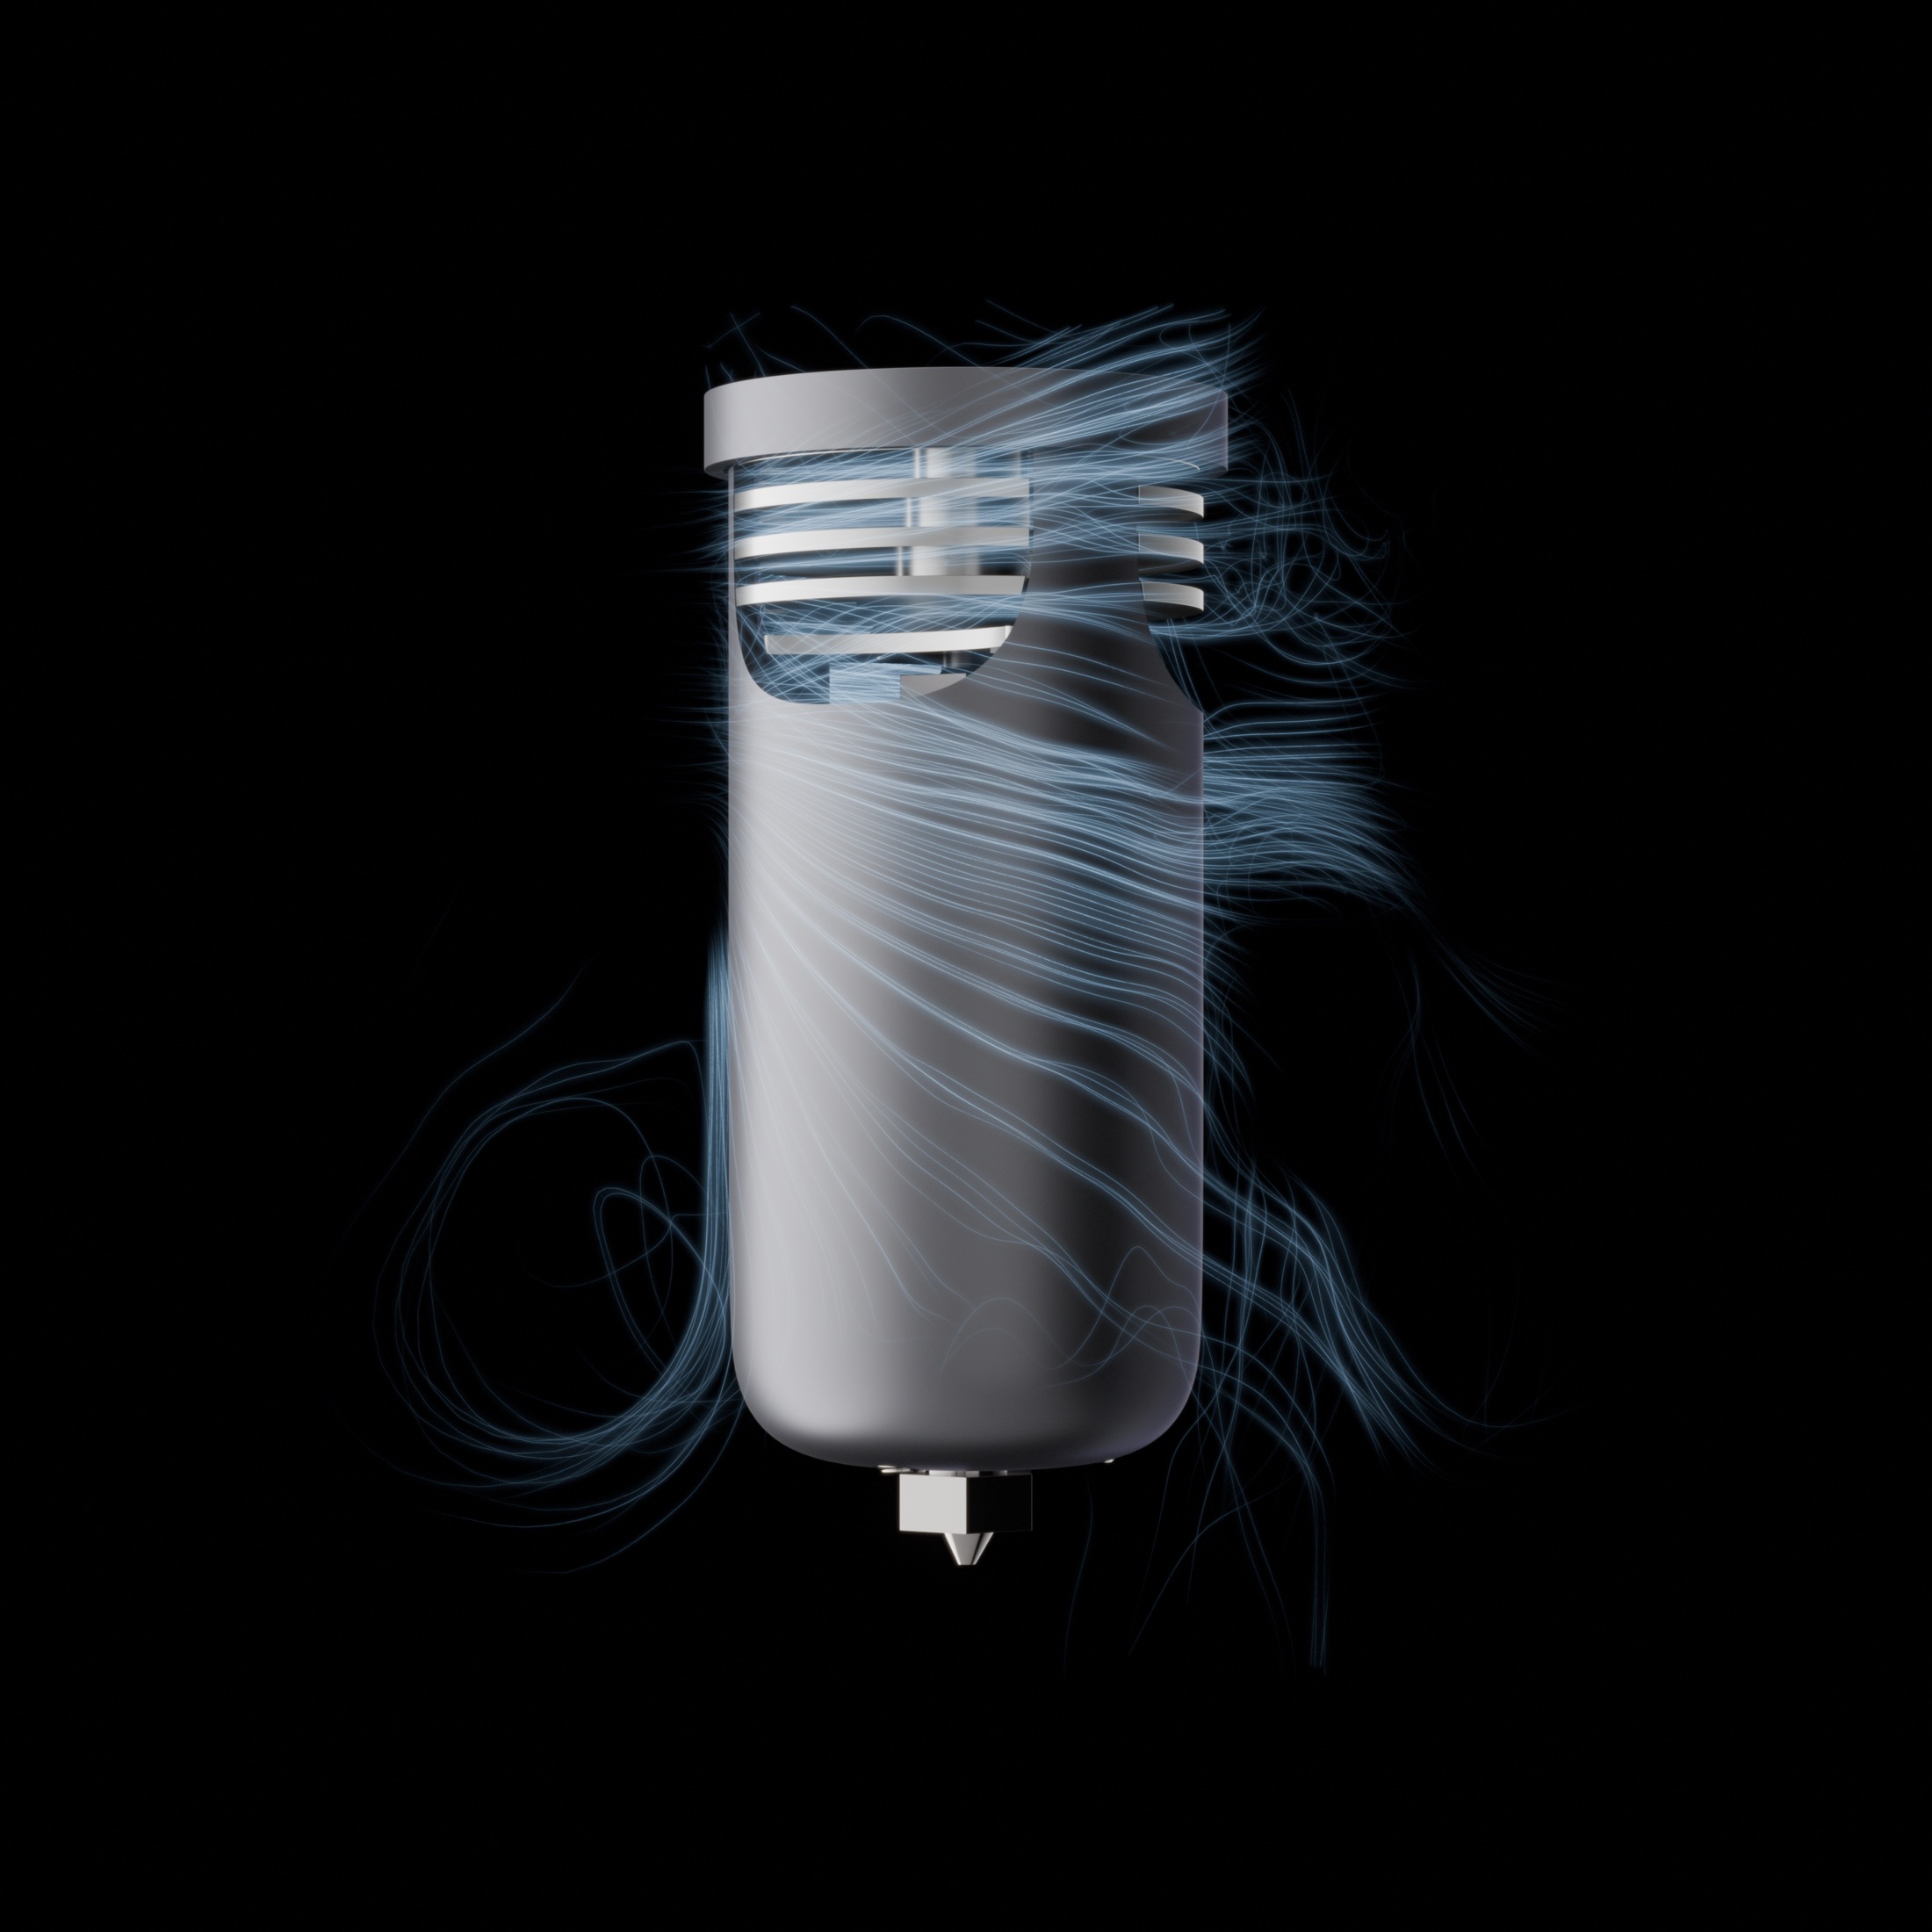
One piece of titanium makes the whole assembly stiff, from the nozzle to the mount.
It keeps the heat in, and the air out.
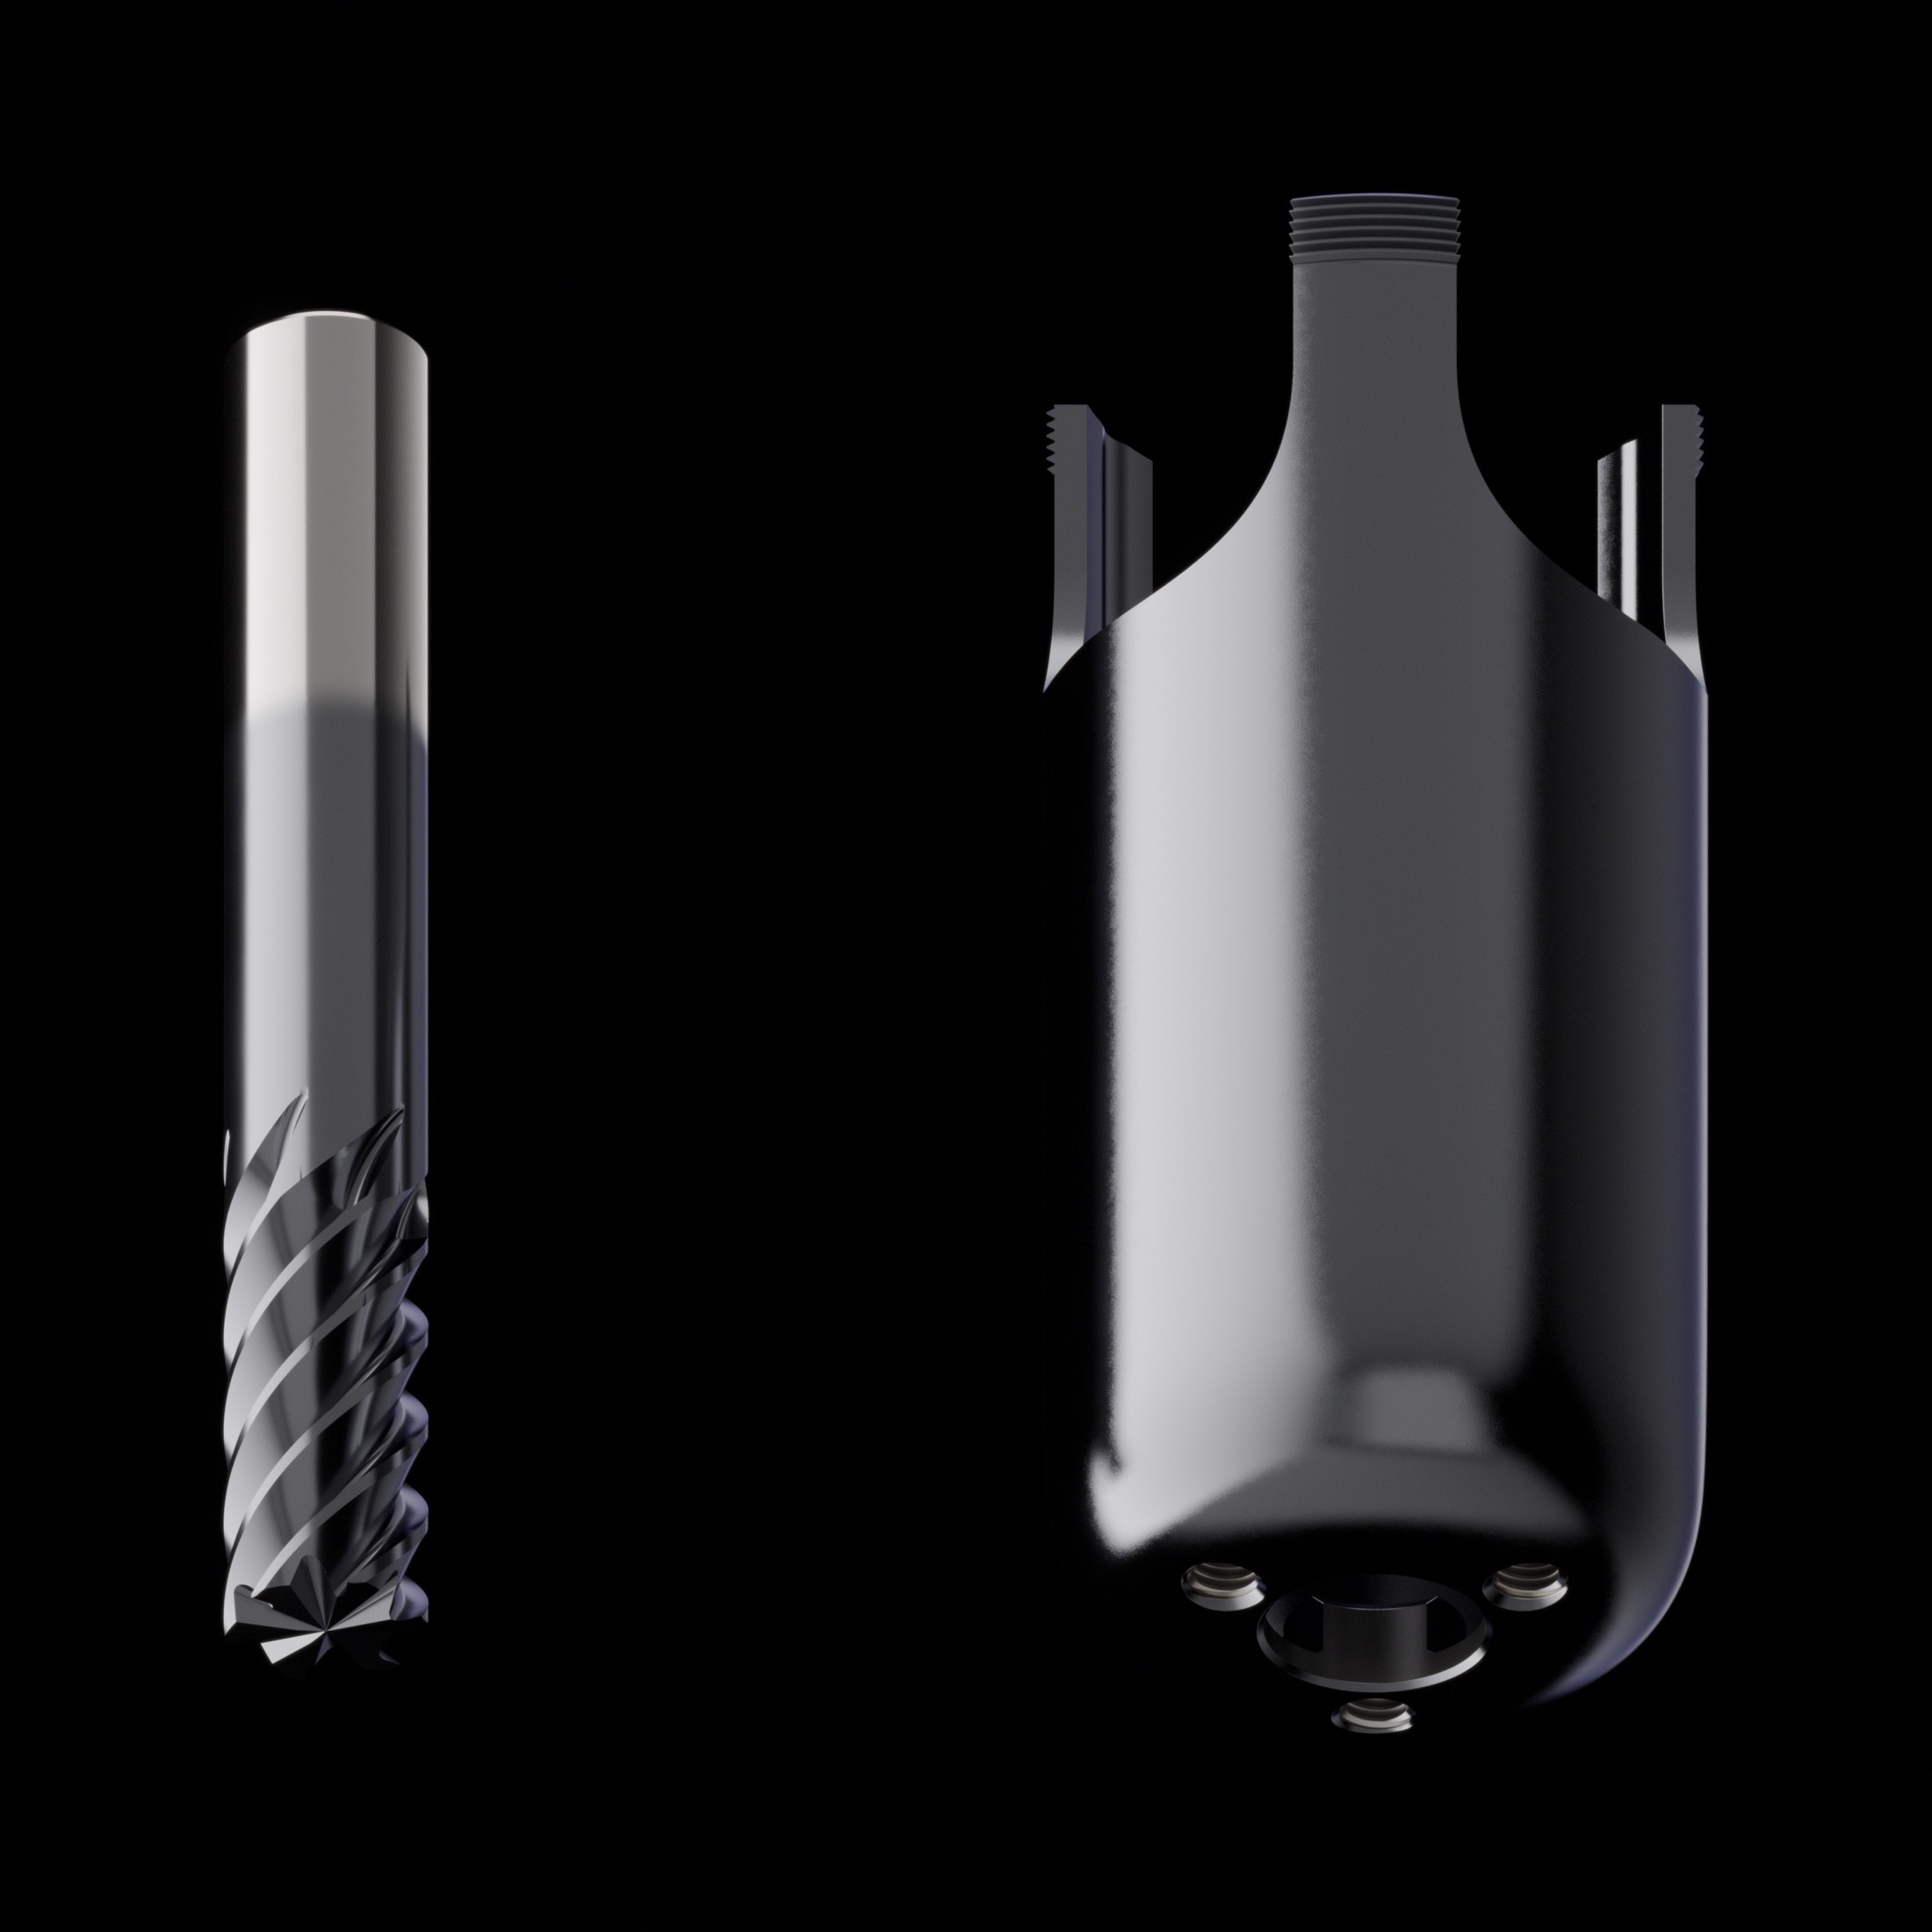
Cutting tools rely on AlTiN to work hot, against hard metal, for a long time.
The shell carries the same coat.
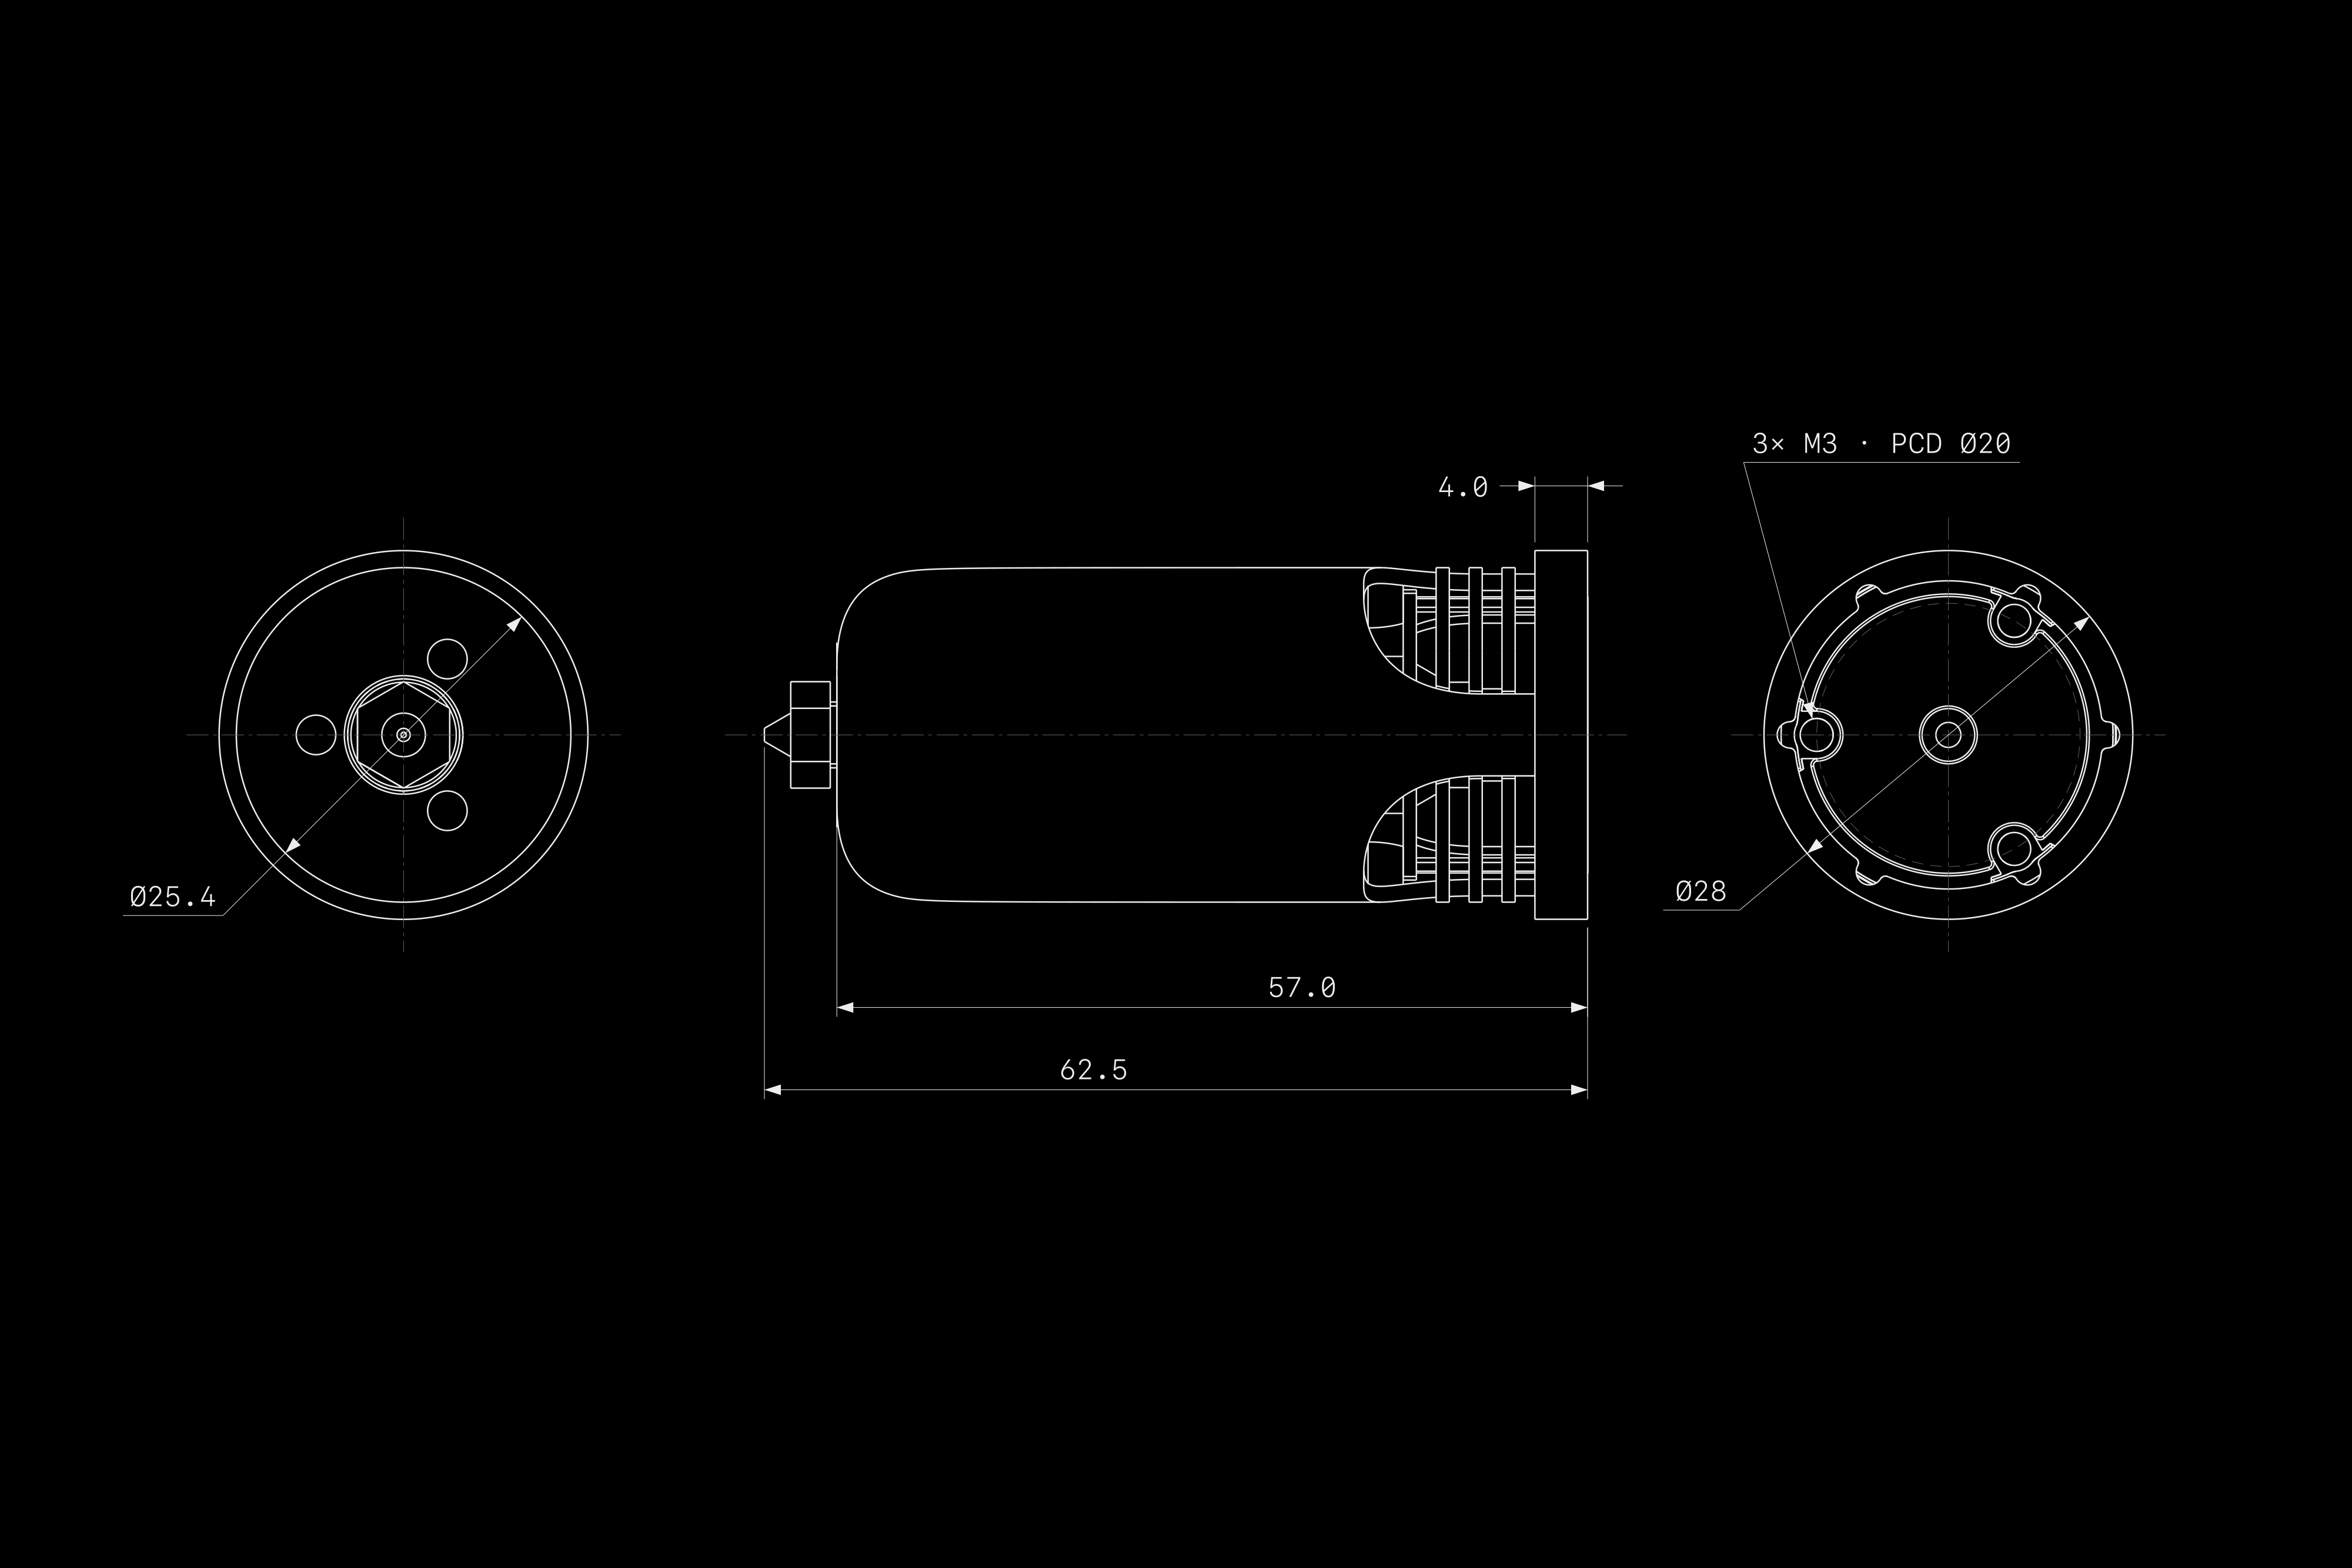
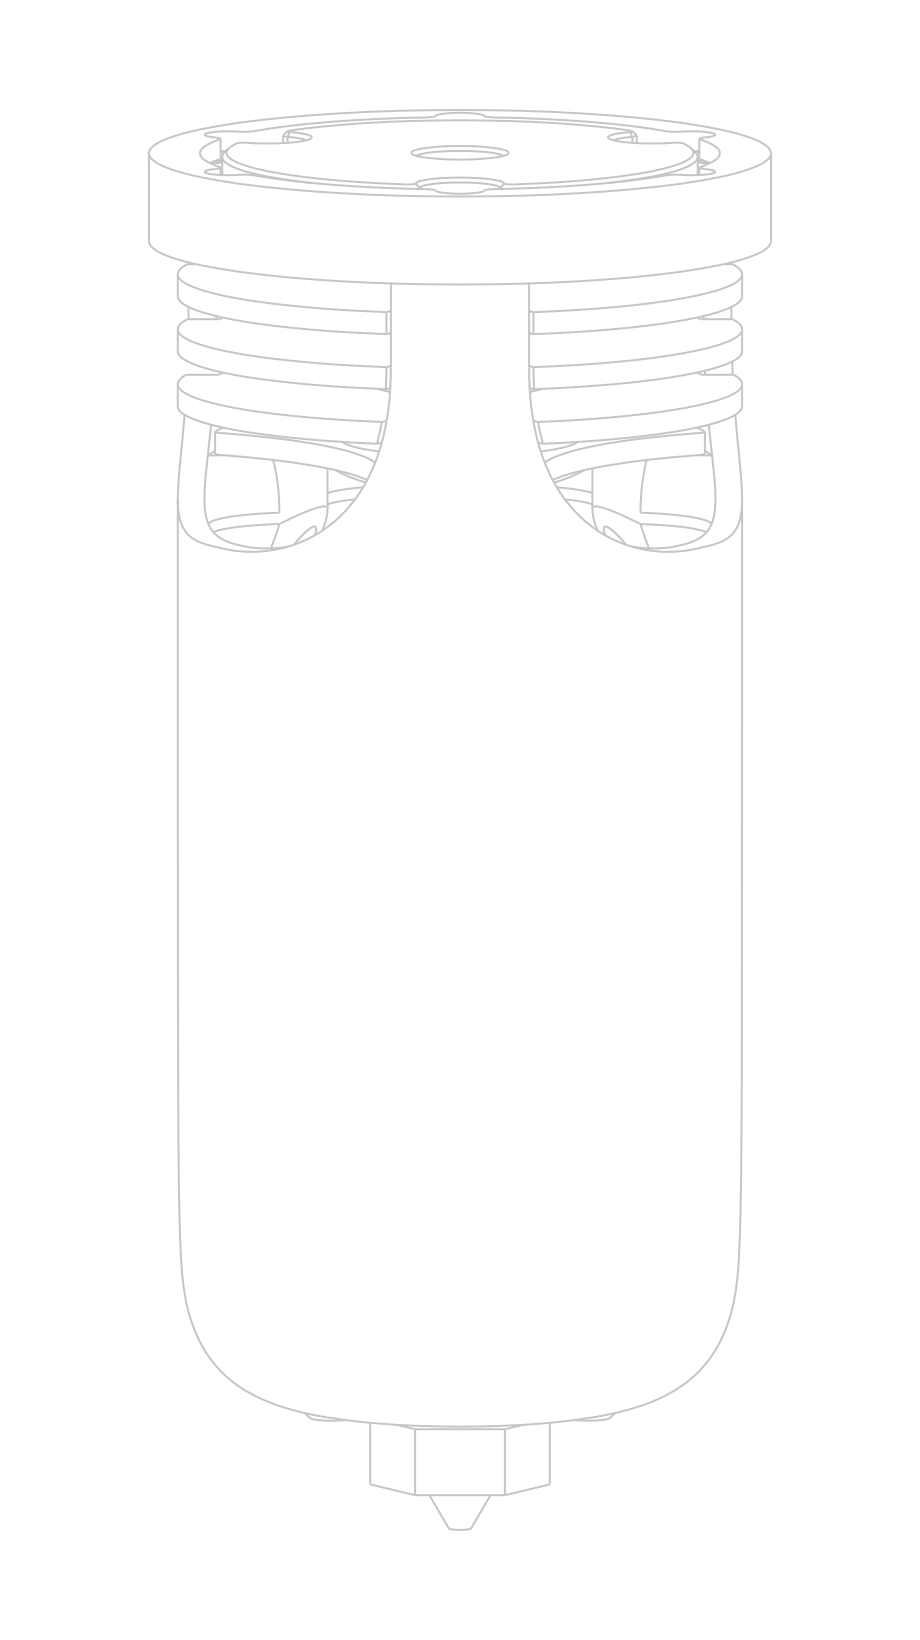
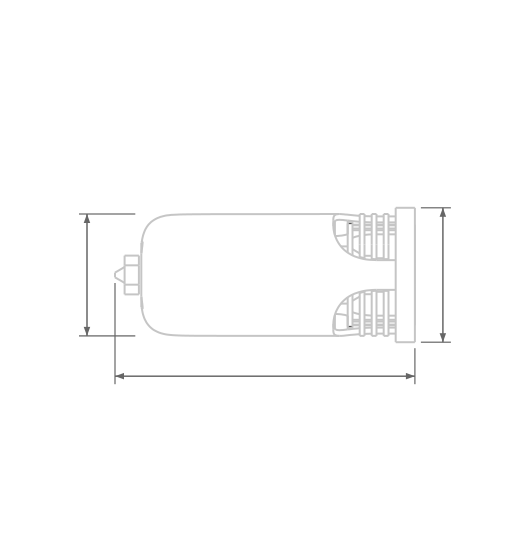 Serious flow in 62.5mmWithout trading away build height.Ø25.4Ø2862.5
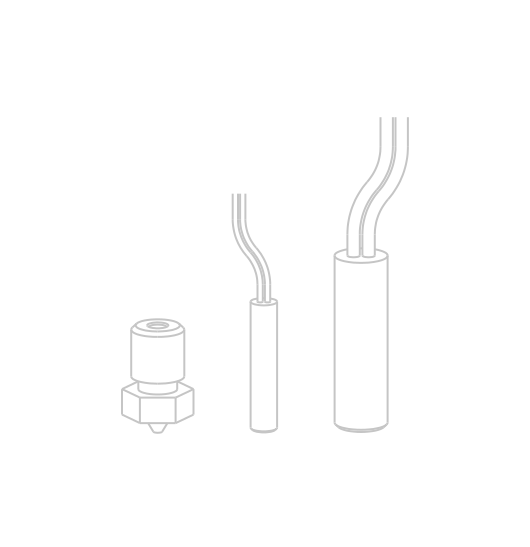 Standard sparesV6 nozzle, Ø6 heaters, Ø3 sensor.
 For most filamentsBuilt for 450 °C.
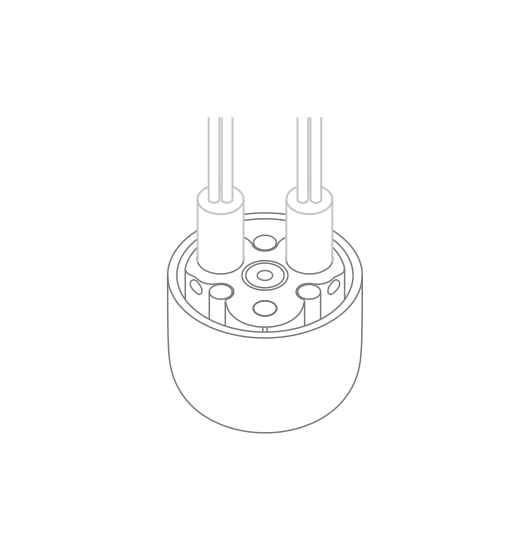 Keeps up with flowLots of power, evenly spread.
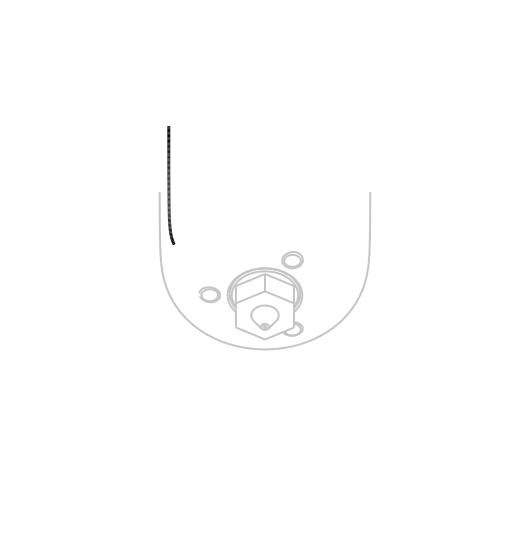 No sharp cornersEasy cleanup around the nozzle.
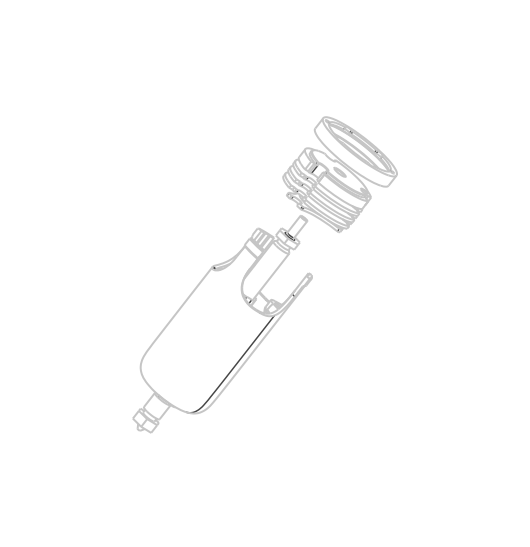 Clean serviceHeaters and sensor isolated.
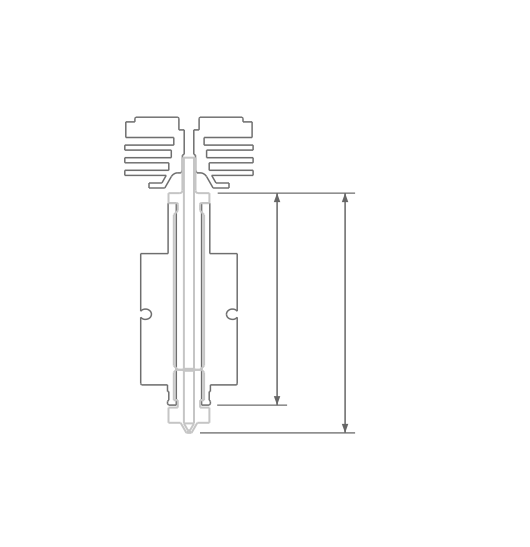 42mm melt zone47.5mm with the nozzle.4247.5
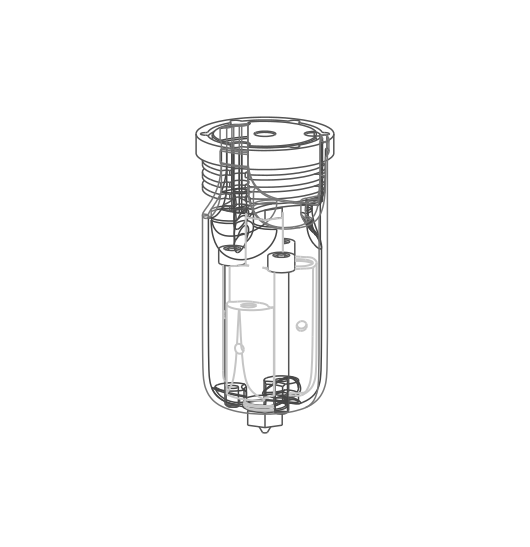 Heat shield by designSteady heat, even at high speed.
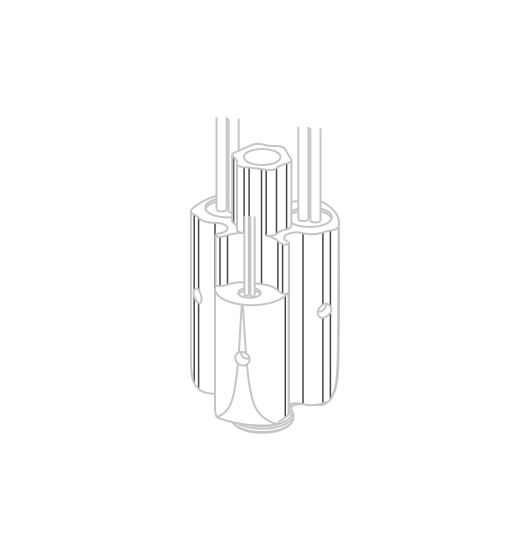
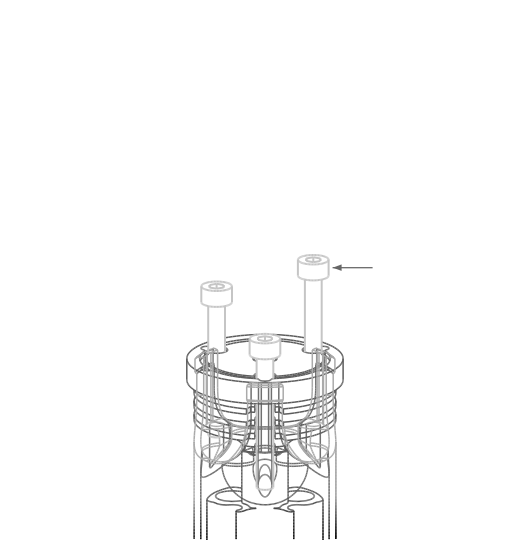 The mount clamps it allThe shell pulls the stack tight.Rigid from end to end.Titanium keeps length stable.3× M3
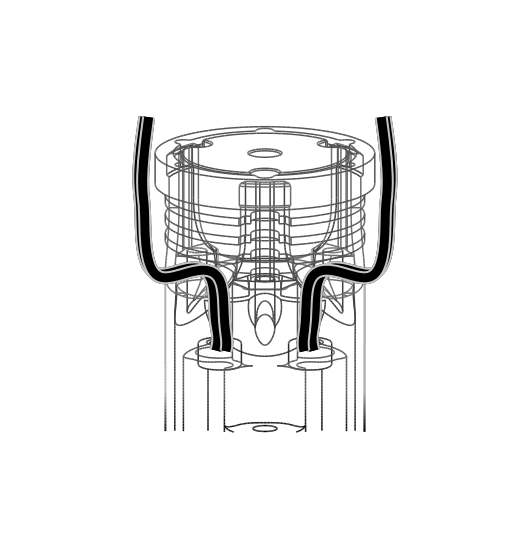 Wires exit at the cold endOut of harm’s way.
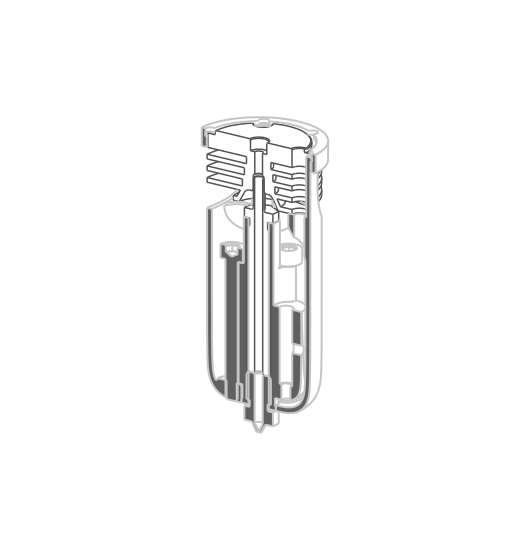 No load on the heat breakProbes and knocks go to the shell.
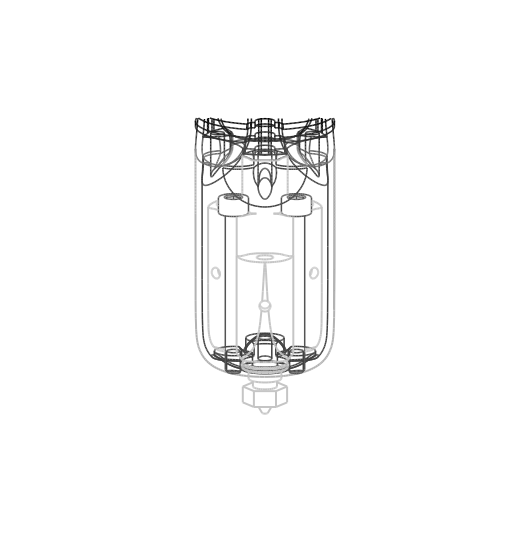 Pit-stop nozzle swapOne hand, the block stays put.